1. Which Carbide Burr Cut Works Best for Cylinder Head Materials?
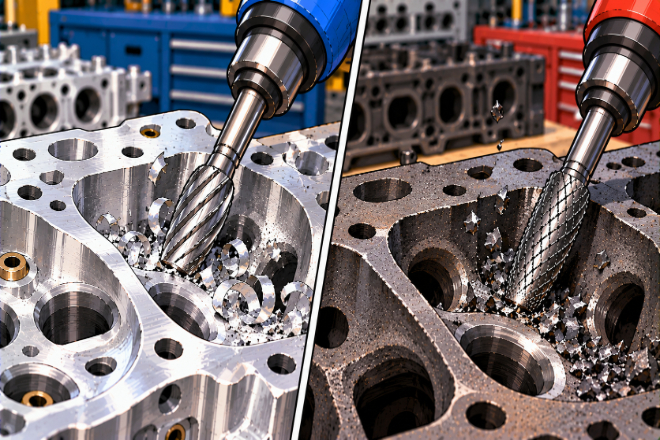
The best carbide burr for cylinder head porting starts with one simple question: What is the cylinder head made from?
Most porting shops commonly deal with aluminum or cast iron cylinder heads.
These two materials behave very differently under a carbide burr, so using exactly the same cutting geometry for both is rarely the best approach.
1). Aluminum Cylinder Heads
Aluminum is soft compared with cast iron, but that does not always make it easier to cut. The real problem is chip loading.
Soft aluminum can produce long, sticky chips. These chips may pack into the teeth of a normal carbide burr.
Once the flutes begin to fill, cutting slows down, heat rises, and the operator starts pushing harder.
That is when a nice porting job can turn into a wrestling match.
For aluminum cylinder head porting, a coarse, open-flute carbide burr designed for aluminum or non-ferrous metals is usually the better starting point.
The wider space between cutting teeth allows larger chips to leave the cutting zone more easily. This is especially useful when removing larger amounts of material from:
Intake ports
Exhaust ports
Port entrances
Bowls
Local casting high spots
2). Cast Iron Cylinder Heads
Cast iron creates a different problem. It is harder and more abrasive than aluminum, so 내마모성 and strong stock removal become more important.
A carbide burr with a cut designed for cast iron can be a strong choice for repeated professional work.
Material-specific CAST geometries are available specifically to improve stock removal and reduce vibration when machining cast iron.
General cross-cut or double-cut burrs can also work, especially when a shop handles many materials and wants a more flexible tool inventory.
The main lesson is simple: Do not choose a cylinder head porting burr only by its shape. Material comes first.
2. Which Carbide Burr Shapes Are Most Useful for Porting?
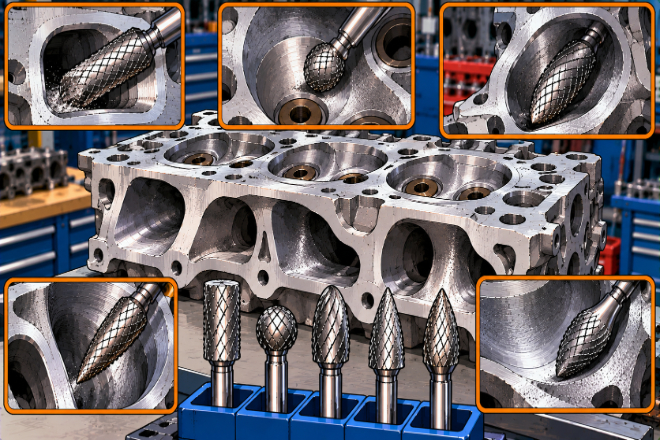
Cylinder head ports are not straight tubes.
They curve, narrow, widen, change direction, and connect several different surfaces. That is why professional porting usually needs more than one carbide burr shape.
A small set of carefully selected shapes can cover most of the work.
3. What Burr Size and Shank Length Should You Choose?
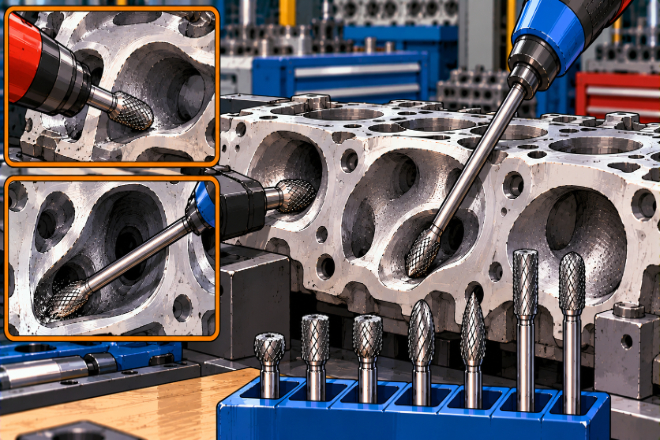
Big burrs remove material quickly. Small burrs provide control. Cylinder head porting usually needs both.
Larger cutting heads can be useful during the early roughing stage, especially around port entrances and open areas where significant material needs to be removed.
But a large burr becomes less useful as the passage becomes tighter. Smaller burrs can work around:
Valve guide areas
Narrow transitions
Tight curves
Local casting defects
Detailed blending areas
The best tool size is therefore not necessarily the biggest burr that fits into the port. It is the burr that gives enough cutting speed while still allowing accurate control.
1). What About Long-Shank Carbide Burrs?
Long-shank burrs are very useful for cylinder head porting because standard burrs may not reach deep enough into the passage.
The longer shank allows the cutting head to reach areas that would otherwise be difficult to access.
But extra reach has a price. As the unsupported shank becomes longer, stiffness decreases. The burr becomes more sensitive to side pressure, bending, and vibration.
Long-shank burrs therefore need:
Rigid tool holding
Controlled pressure
Stable cutting
Careful speed selection
Minimum practical extension
Do not use extra length just because it looks convenient. Use it because the port actually requires it.
For professional shops, keeping both standard-length and long-shank carbide burrs available usually makes more sense than trying to perform every porting operation with one tool.
4. Should You Use Aggressive or Fine-Cut Burrs?
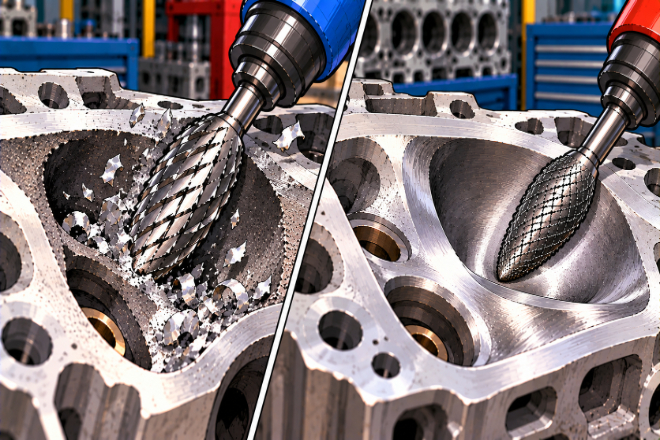
Cylinder head porting is not one cutting operation. It is a series of controlled material-removal steps.
Early in the process, the shop may need to remove casting material quickly. Later, the goal changes to shaping transitions and controlling the final geometry.
That makes a two-stage tool strategy useful.
1). Roughing Stage
For rough material removal, an aggressive material-specific burr can save considerable time.
On aluminum, this usually means an open-flute design that clears chips effectively.
On cast iron, a dedicated cast-iron cut or suitable aggressive carbide burr can provide faster stock removal.
The purpose here is not to create the final surface. It is to reach the basic shape efficiently.
2). Controlled Shaping Stage
As the port approaches its target geometry, control becomes more important than raw removal speed.
A less aggressive burr, smaller diameter, or different shape can help blend surfaces without removing too much material.
This is where many porting jobs go wrong. The operator becomes comfortable with an aggressive burr and continues using it too close to the final dimensions.
A carbide burr can remove metal much faster than it can put it back. Professional porting therefore needs a clear point where roughing stops and controlled shaping begins.
Carbide burrs also do not need to produce the final polished surface in every application. Abrasive rolls, cartridge rolls, or other finishing tools may follow the carbide stage when a finer finish is required.
The burr creates the geometry. Finishing tools refine the surface. Those are related jobs, but they are not exactly the same job.
5. How Can You Avoid Removing Too Much Material?
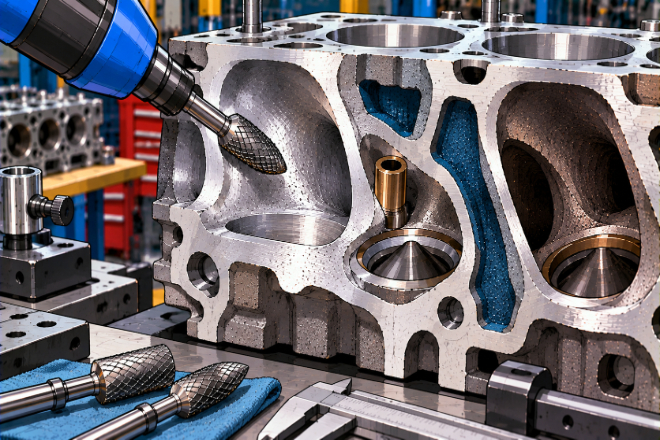
Cylinder head porting is not simply about making the ports bigger. This is one of the most important ideas in the entire process.
The goal is controlled reshaping based on the engine design and the performance target. Removing material without a plan can change port velocity, cross-sectional area, wall thickness, and flow behavior.
Some areas also sit close to water passages, valve seats, guides, or other critical features. Once too much metal is gone, the carbide burr has no undo button.
Professional shops therefore use measurement and repeatability rather than relying only on visual judgment.
Depending on the work, this may include:
Port templates
캘리퍼스
Thickness measurements
Reference heads
CNC data
Flow testing
Marked target areas
The burr should remove only the material required by the porting plan. This is also why burr shape matters so much.
A large cylindrical tool can be excellent for an open wall but awkward around a tight short-side curve. A ball or oval burr may give much better control there.
The same applies near valve guide areas. Use a tool that can approach the feature naturally rather than forcing a large cutting head into a small space.
Critical valve seats and other precision surfaces should not become casual carbide-burr territory. Those features need the correct dedicated machining process.
Porting skill is not measured by how quickly metal disappears. It is measured by how accurately the right metal disappears.
6. What Should a Professional Porting Shop Look for When Buying Burrs?
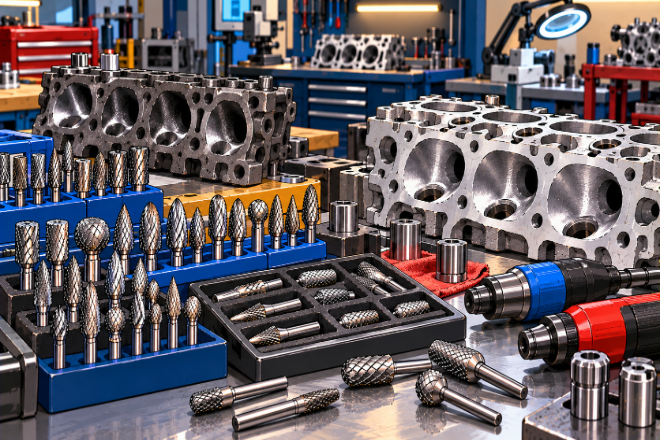
For an engine shop, the best carbide burr is not necessarily the cheapest one in the catalog.
Porting work can keep a burr in use for long periods, often in deep and awkward passages. Tool quality therefore affects much more than purchase price.
Important factors include:
1). Concentricity
A burr that rotates accurately can help reduce vibration and chatter marks. Poor concentricity makes controlled shaping more difficult and can increase wear on both the burr and grinder.
2). Carbide quality
The cutting head needs enough wear resistance to maintain useful edges through repeated work.
3). Cut consistency
If several burrs of the same type behave very differently, process control becomes difficult.
4). Shank quality
This becomes especially important with extended-reach tools.
5). Material-specific options
Shops working on many aluminum heads may benefit from dedicated aluminum cuts, while businesses handling older cast-iron heads may need strong cast-iron options.
A useful professional porting set might include:
Open-cut burrs for aluminum
Cast-iron or suitable cross-cut burrs for iron heads
Cylindrical radius-end shapes
Ball and oval shapes
Tree or flame shapes
Several head diameters
Standard and long-shank versions
Do not judge the set by how many burrs are inside the box. Judge it by how many porting operations those burrs can perform well.
For production or specialist performance shops, test new burrs on real cylinder head materials. Compare stock removal, loading, vibration, control, tool life, and surface condition.
The winning tool is the one that helps the shop create the intended port geometry repeatedly without turning every cylinder head into an experiment.
 English
 Español
 简体中文
 Français
 日本語
 한국어
 العربية
 Tiếng Việt