1. Why Do Tungsten Carbide Burrs Create Rough Surfaces?
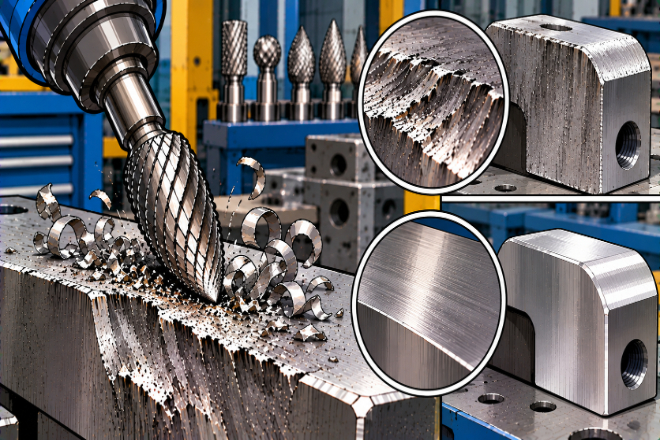
قواطع كربيد التنغستن are designed to cut metal quickly.
They are often used in industries where fast material removal is needed, including السيارات manufacturing, الفضاء الجوي, mold repair, welding fabrication, and general machining.
However, fast cutting does not always mean a smooth finish. A rough surface usually means that the cutting process is not balanced.
The burr may remove material too aggressively, create uneven contact, or damage the surface during cutting.
Common reasons include:
Wrong burr cut style
Incorrect RPM
Too much pressure
Worn cutting teeth
Wrong burr shape
Poor tool control
Material problems
A tungsten carbide burr works differently from a traditional grinding tool.
The cutting teeth remove small pieces of material as the burr rotates. When these teeth work correctly, they create a controlled surface.
When the cutting action becomes unstable, the surface quality decreases. For companies using carbide burrs in production or maintenance, surface finish is important.
A rough surface can create additional problems:
Extra polishing work
Poor part appearance
Difficult assembly
Reduced sealing performance
More production time
For example, a company repairing a pump housing may use a carbide burr to remove damaged material before welding.
If the burr leaves deep marks, the repair area may need additional finishing. This increases labor cost. The goal is not simply removing material.
The goal is removing material while maintaining acceptable surface quality. Understanding why rough surfaces happen is the first step to improving results.
2. How Does Burr Cut Style Affect Surface Finish?
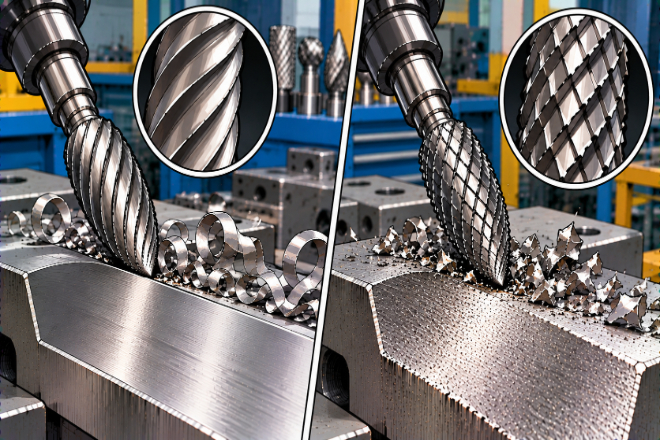
One of the biggest factors affecting surface quality is the burr cut style. Different cuts are designed for different purposes.
Some cuts focus on fast material removal. Others focus on smoother finishing. The most common types include:
قطع واحد
Double cut
Aluminum cut
Fine cut
A single-cut carbide burr usually has fewer cutting edges. This design allows strong chip removal and smooth cutting action.
It is often used for:
General shaping
Stainless steel work
Long chip materials
Controlled finishing
A double-cut carbide burr has crossing teeth. This creates smaller chips and more cutting edges.
It is commonly used for:
General deburring
Smoother surface results
Reduced vibration
Better operator control
However, double-cut does not automatically mean perfect finishing.
The final result depends on:
مادة
RPM
ضغط
Tool movement
For example, using a rough material removal burr on a final finishing step may leave visible marks.
A simple comparison:
3. Can Incorrect RPM Cause a Rough Surface?
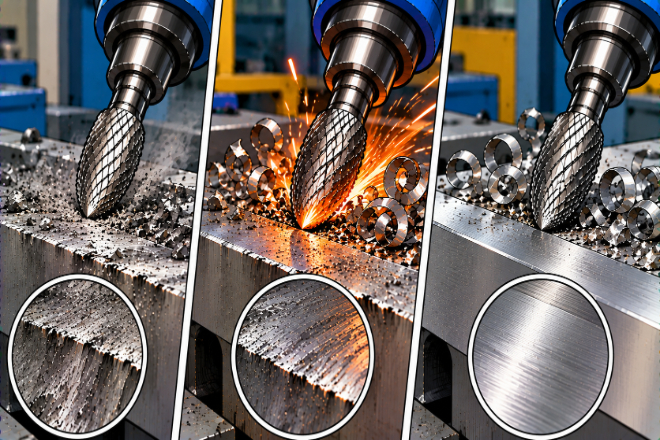
Yes. RPM has a direct effect on surface quality. A carbide burr needs the correct speed to cut smoothly.
When RPM is too low, the burr may not cut properly. The teeth may rub against the surface instead of removing material efficiently.
This creates:
Uneven marks
زيادة الاهتزاز
Poor cutting performance
When RPM is too high, another problem appears. The burr can generate excessive heat.
High heat may cause:
عمر أداة منخفض
Material discoloration
الضرر السطحي
Unstable cutting
The correct RPM depends on:
Burr diameter
Material type
Cutting style
طلب
A larger burr usually requires a lower RPM. A smaller burr can normally operate at a higher speed.
For example, using a large carbide burr at the same speed as a small burr can create excessive surface speed and increase roughness.
Many companies make the mistake of increasing RPM when they want faster production. However, faster is not always better.
A stable cutting process often produces better results than maximum speed. For decision-makers, the goal should be:
Better surface quality with efficient tool usage. Not simply the fastest rotation speed.
4. How Does Excessive Pressure Affect Surface Quality?
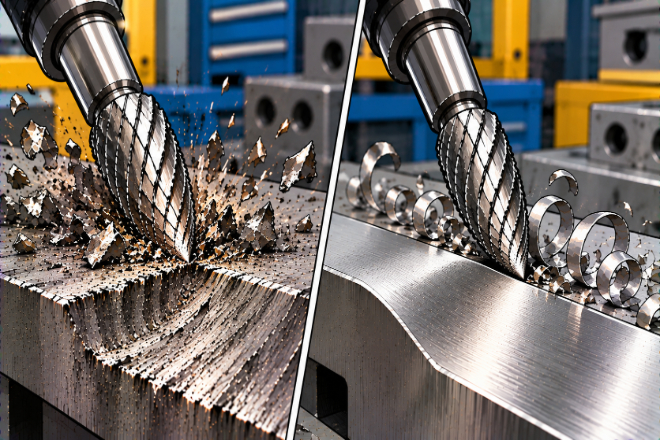
Pressure is another common reason carbide burrs leave rough surfaces. Many operators believe more pressure means faster cutting.
In reality, carbide burrs are designed to cut through rotation. They do not need heavy force.
Too much pressure can cause:
Burr skipping
Surface scratches
Uneven cutting
Excessive heat
Faster tool wear
When the operator pushes too hard, the burr cannot work naturally. The cutting teeth become overloaded. Instead of creating smooth chips, the tool tears at the surface.
This creates a rough finish. A better method is to use steady and controlled movement. The operator should guide the burr and allow the teeth to remove material.
This is especially important for:
الفولاذ المقاوم للصدأ
الألومنيوم
التيتانيوم
Hardened alloys
Different materials respond differently to pressure. Training operators to use the correct force can significantly improve surface quality.
For automated systems, pressure control is even more important. Robotic deburring requires stable settings because the machine cannot adjust based on feeling.
The correct combination of feed rate and cutting force creates repeatable results.
5. How Does Burr Shape Influence Surface Finish?
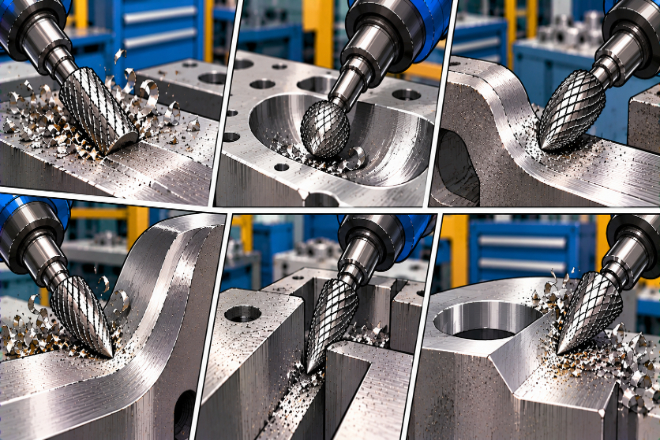
Burr shape affects how the tool contacts the workpiece. Using the wrong shape can create uneven cutting.
Common carbide burr shapes include:
Cylindrical
Ball
Oval
Flame
Tree
Cone
A cylindrical burr works well for flat areas. A ball burr is useful for curved surfaces. A flame burr works well for narrow profiles. A tree burr can reach corners and internal areas.
The wrong shape can concentrate cutting force in a small area. For example, using a cylindrical burr on a curved surface may create uneven contact.
Some areas receive more cutting force than others. This creates rough spots. The correct burr shape allows smoother movement and more stable cutting.
For companies working with complex parts, burr selection should consider:
Surface shape
Access area
Required finish
Material type
The best burr is not always the one that removes the most material. It is the one that matches the application.
6. Can a Worn Carbide Burr Create Rough Finishes?
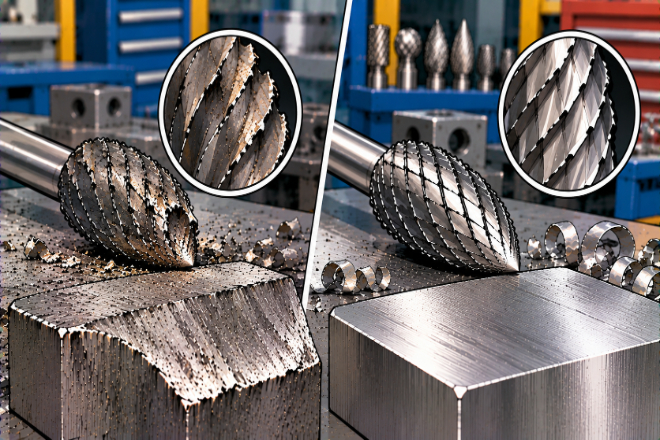
Yes. A worn burr often produces poor surface quality. Over time, carbide cutting teeth lose their sharp edges.
The burr may still remove material, but the cutting action becomes less controlled.
Signs of a worn carbide burr include:
زيادة الاهتزاز
More noise
Slow cutting
Rough surface
Higher pressure requirement
Some companies continue using worn burrs because the tool can still cut. However, this can increase total costs.
A worn burr may create:
More finishing work
Longer production cycles
Higher labor costs
Lower product quality
Regular inspection is important.
Check:
Tooth condition
Cutting performance
Surface results
Vibration level
Replacing a burr at the correct time often saves more money than using it until failure.
7. How Can Companies Improve Carbide Burr Surface Finish?
Improving surface finish requires a complete process approach. Companies should focus on several areas:
1). Select the Correct Burr
Choose the burr based on:
مادة
Cut style
Shape
Required finish
2). Optimize Cutting Conditions
Control:
RPM
ضغط
Feed speed
Tool angle
3). Maintain Equipment
Check:
Collets
Holders
Rotary tools
Spindles
Poor equipment condition can create vibration and unstable cutting.
4). Train Operators
Operators should understand that carbide burrs need controlled movement. Too much force usually creates worse results.
5). Test Before Production
Before large-scale use, test:
Surface quality
عمر الأداة
سرعة القطع
Final appearance
A small adjustment can often create a large improvement.
For manufacturers, better surface finish means:
Less rework
Lower costs
جودة المنتج أفضل
More stable production
 English
 Español
 简体中文
 Français
 日本語
 한국어
 العربية
 Tiếng Việt