1. Why Do Tungsten Carbide Burrs Vibrate During Use?
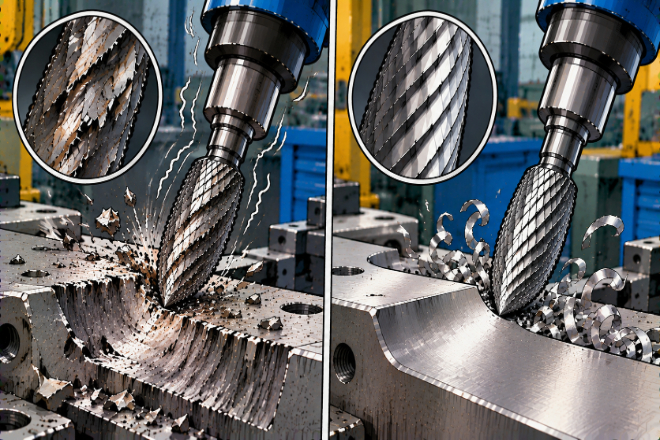
Tungsten carbide burrs are popular because they can remove metal quickly and work on many difficult materials.
They are used in industries such as automotive, aerospace, mold making, welding repair, and general manufacturing.
However, even a high-quality carbide burr can vibrate if the cutting conditions are not correct. Vibration happens when the cutting force is not stable.
During operation, the burr rotates at high speed while the cutting teeth contact the material. Ideally, the tool should cut smoothly and continuously. But when the contact changes too much, the burr starts to move back and forth.
This creates vibration. Common causes include:
Incorrect RPM
Too much cutting pressure
Wrong burr shape
Poor tool holding
Excessive overhang
Damaged burr teeth
Unstable workpiece
At first, vibration may seem like only a comfort problem. The tool feels harder to control. The noise becomes louder. The operator may need more effort.
But the real impact is much bigger. For manufacturers, vibration can lead to:
Shorter carbide burr life
Higher tool costs
Poor surface finish
More rework
Longer production time
A small vibration problem repeated across thousands of parts can become a serious manufacturing issue.
This is why reducing vibration is not only about making the operator more comfortable. It is about improving the whole process.
The good news is that most vibration problems can be reduced without changing the entire system.
Small improvements in tool selection, machine settings, and working methods can create noticeable results.
2. How Does RPM Affect Carbide Burr Vibration?
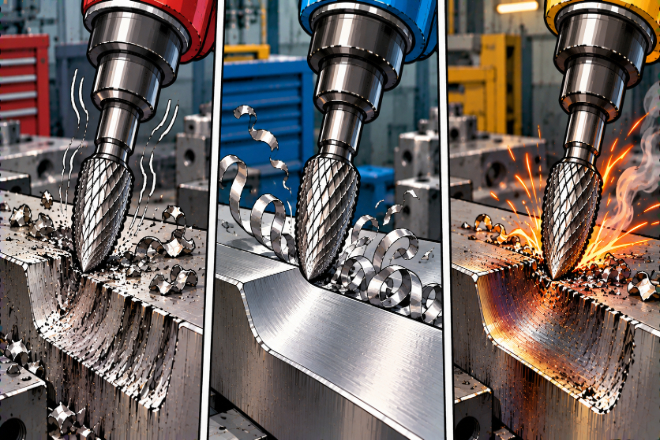
RPM is one of the first factors to check when vibration appears.
A tungsten carbide burr needs the correct rotational speed to work properly. If the speed is too low, the burr may not cut effectively.
Instead of cutting, the teeth may rub against the material. The operator may push harder to get better results, which creates more vibration.
If the speed is too high, the cutting area can become unstable.
High speed can increase:
Heat
Tool wear
Cutting pressure
Surface damage
The correct RPM creates a balance between cutting ability and stability.
The ideal speed depends on:
Burr diameter
Material type
Burr cut design
Machine power
Application
A larger burr usually requires a lower RPM because the cutting surface travels faster. A smaller burr can normally operate at higher speeds.
A basic guide:
3. Can Too Much Pressure Increase Carbide Burr Vibration?
Yes.
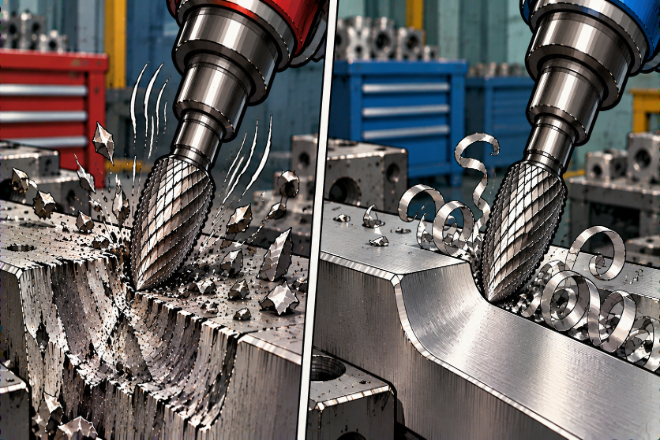
Excessive pressure is one of the most common reasons carbide burrs vibrate. Many users believe that pushing harder will remove material faster.
In reality, carbide burrs work best when the cutting teeth can freely remove material. Too much force creates several problems:
Increased vibration
Higher heat
Faster tooth damage
Poor surface quality
Reduced tool life
When the operator pushes too hard, the burr cannot cut smoothly. The cutting edges start hitting the surface instead of slicing through the material.
This creates an unstable cutting action. A better method is to guide the tool with controlled pressure. Let the carbide teeth do the work.
For production environments, this is especially important because different operators may use different force levels.
A skilled operator may naturally adjust pressure. However, automated systems and less experienced workers need clear process settings.
Companies can reduce vibration by creating simple operation standards:
Recommended pressure range
Correct RPM
Proper burr angle
Maximum tool contact area
A carbide burr is not a hammer. It is a cutting tool. Treating it like a hammer is usually the fastest way to create vibration.
4. How Do Tool Holding and Overhang Influence Vibration?
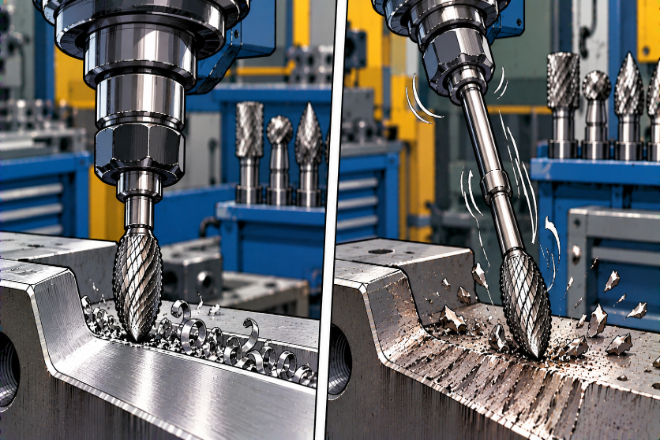
The connection between the burr and the machine has a major effect on stability.
A perfectly designed carbide burr can still vibrate if it is not held correctly. Several setup problems can increase vibration.
1). Poor Collet Condition
The collet holds the burr during rotation. If it is worn, dirty, or damaged, the burr may not rotate evenly. This creates imbalance.
2). Excessive Tool Overhang
Overhang is the distance between the holder and the cutting area. A longer burr extension can help reach difficult locations.
However, too much extension reduces stiffness. The tool behaves like a longer lever and becomes easier to move.
The result is more vibration. Use the shortest burr length that can safely reach the working area.
3). Incorrect Installation
The burr should be installed correctly inside the holder.
Poor installation can cause:
Tool movement
Uneven rotation
Increased wear
For high-speed applications, proper installation is not optional.
It directly affects performance. Manufacturers should regularly check:
Collet condition
Holder condition
Burr installation
Spindle accuracy
Many vibration problems are not caused by the burr itself. They are caused by the system holding the burr.
5. How Does Burr Shape Affect Cutting Stability?
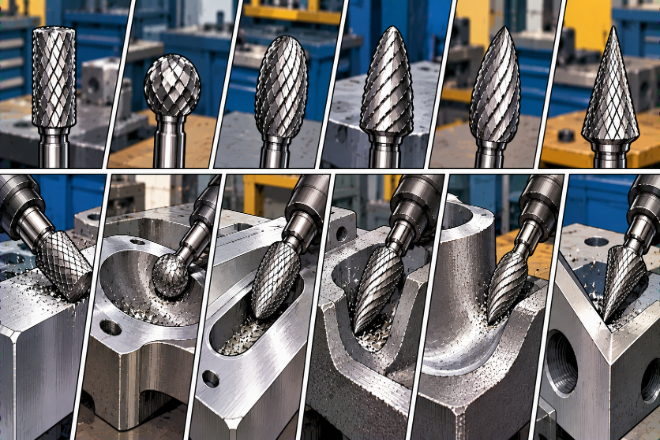
Choosing the correct burr shape can greatly reduce vibration. Different shapes create different contact patterns.
A burr that matches the surface geometry will usually cut more smoothly. Common carbide burr shapes include:
Cylindrical
Cylindrical radius-end
Ball
Oval
Tree
Flame
Cone
A cylindrical burr works well on flat surfaces. A ball burr is better for curved areas. A flame burr can reach narrow spaces and changing profiles. A cone burr works well for angled areas.
Using the wrong shape can create unstable contact. For example, using a flat cylindrical burr on a curved surface means only a small area touches the material.
The cutting force becomes concentrated. This increases vibration. The correct shape spreads the cutting action more evenly.
For companies working with complex components, selecting the right burr shape is often more important than choosing the most aggressive cutting tool.
A stable cutting process usually produces better results than maximum material removal speed.
6. How Can Damaged Carbide Burrs Create Vibration?
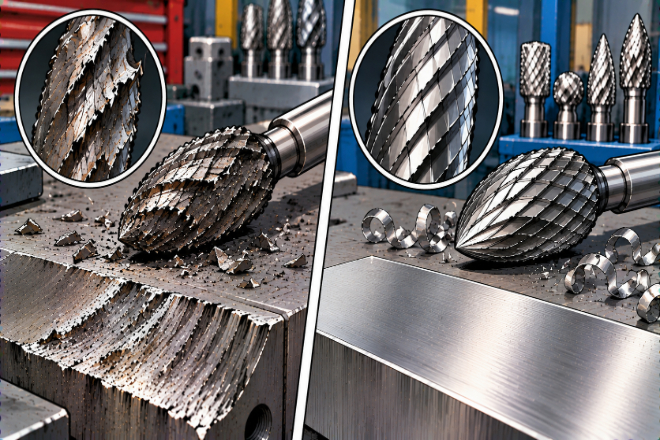
Sometimes vibration starts because the burr is already worn. A damaged carbide burr cannot cut evenly.
The cutting teeth may no longer contact the material in a balanced way.
Common signs include:
Increased noise
Stronger vibration
Poor surface finish
Slower cutting
Visible tooth damage
Some operators continue using worn burrs by increasing pressure. This usually creates more problems.
The worn tool produces more heat and vibration, while the operator spends more time completing the same task. Regular inspection helps prevent this.
Before use, check:
Cutting edge condition
Burr surface
Shank damage
Previous performance
A burr should be replaced when it no longer produces the required result.
Tool cost is only one part of manufacturing cost.
A damaged burr can create:
More labor time
More rework
More downtime
Lower product quality
Replacing a small cutting tool at the right time can protect much larger production costs.
7. How Can Companies Reduce Vibration in Daily Production?
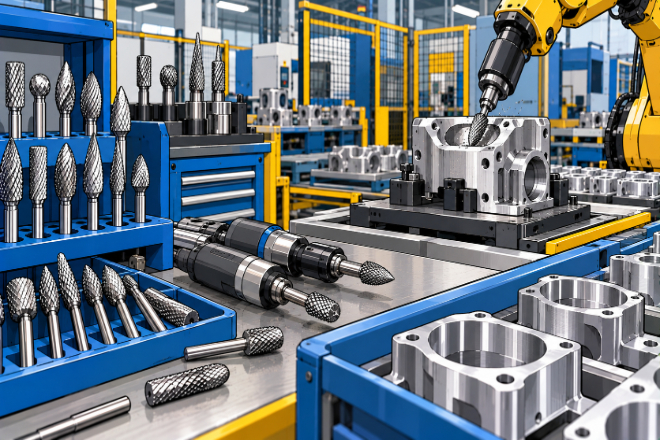
Reducing vibration requires a complete approach. Changing only the burr is not always enough. Companies should review the entire cutting process.
1). Select the Correct Burr
Choose based on:
Material
Shape
Cutting requirement
Surface finish
2). Control Machine Settings
Check:
RPM
Feed rate
Cutting direction
Contact pressure
3). Improve Tool Maintenance
Maintain:
Collets
Holders
Spindles
Rotary tools
4). Train Operators
Operators should understand that controlled cutting creates better results than excessive force.
5). Test Before Full Production
For automated or high-volume applications, test different settings before starting full production.
Compare:
Vibration level
Tool life
Surface quality
Cycle time
The best process is not always the fastest cutting process.It is the process that creates stable and repeatable results.
For decision-makers, reducing vibration can improve:
Production efficiency
Tool cost control
Product quality
Equipment life
Small improvements in tool stability often create large improvements over time.
 English
 Español
 简体中文
 Français
 日本語
 한국어
 العربية
 Tiếng Việt